by Kheeran Offshore Technical Team Kheeran Offshore Technical Team

Ultrasonic Flaw Detection for Weld Metal

A certificate alone does not solve a technical problem. With Ultrasonic Flaw Detection for Weld Metal, the result must be traceable to the right item and interpreted against the right requirement. That is the standard our team applies from the first review.

The work may involve one sample, one inspection visit, or a planned series of activities. In every case, we keep identification and reporting connected from the start. A project team should be able to follow the record without guessing what was examined.

NDT works best when the method is chosen for the expected discontinuity, material, geometry, access, and surface condition. A method that is excellent for one weld may be unsuitable for another.

Before the inspector or sample arrives: Ultrasonic Flaw Detection for Weld Metal

First, we review the available drawings, purchase documents, procedures, sample details, and previous records. The team then confirms the applicable requirement, the area or item to be covered, and the acceptance basis. We list missing information before work begins.

Next, project conditions matter. Access, permits, production status, safe isolation, sample preparation, witness notice, and turnaround time can affect the plan. Agreeing these points early keeps the assignment realistic.

How the work is controlled

During the assignment, qualified personnel follow the approved method and record the conditions that can influence the result. The exact controls depend on the service, but the aim stays the same: make every observation or measurement traceable to the correct item.

  • scope and acceptance criteria
  • equipment calibration
  • surface condition and access
  • technician qualification
  • scan or examination coverage
  • indication evaluation and reporting

For example, typical risks include wrong method selection, insufficient coverage, poor calibration control. We also manage these risks through identification checks, suitable equipment, clear hold points, and timely communication with the client.

Most importantly, the work follows the specified ASTM, ASME, API, ISO, AWS, class, or client procedure. If the contract uses a different requirement, the approved project document takes priority. We document coverage and acceptance against the stated procedure and code.

What clients often ask us

Which NDT method should be requested?

Share the component, material, thickness, weld geometry, access, code, and suspected condition. We can then confirm whether VT, PT, MT, UT, PAUT, TOFD, or another method fits the scope.

For this reason, providing this information at the enquiry stage helps us quote the correct work. It also reduces last-minute changes once we have reserved personnel, equipment, or laboratory time.

What the final record should show

Finally, the report identifies the item, its origin, the method, and the finding. Depending on the scope, the supporting record may include equipment details, calibration checks, examination maps, indication data, results, and technician identification. We state any limitation or deviation plainly.

However, if a result does not meet the requirement, we identify the affected item and communicate the finding. The client can then decide whether to repair, replace, investigate, or request further verification. We record the agreed close-out action when it forms part of our scope.

Support for projects in Guyana

In Guyana, Kheeran Offshore supports oil and gas, offshore and marine, energy, fabrication, manufacturing, construction, and infrastructure work. Assignments may take place at vendor facilities, fabrication yards, operating sites, offshore assets, or our Georgetown laboratory, depending on the service.

Depending on the need, the scope can cover a single urgent item or a planned inspection and testing programme. In both cases, the client receives one local point of contact and a report written for practical project use.

Request Ultrasonic Flaw Detection for Weld Metal in Guyana

Contact Kheeran Offshore to discuss Ultrasonic Flaw Detection for Weld Metal. Call or WhatsApp +592-602-5664, email admin@kheeran.gy, or use our contact page. Please include the item, location, applicable requirement, schedule, and expected deliverable. We will review the details and prepare a clear quotation.
by Kheeran Offshore Technical Team Kheeran Offshore Technical Team

Piping Welding Inspection and NDT Services in Guyana

Reliable piping welding inspection and NDT Guyana gives project teams clear evidence about weld quality. Kheeran Offshore supports piping fabricators, EPC contractors, plant owners, and commissioning teams across Guyana. We inspect process piping, fabricated spools, field tie-ins, repairs, and pressure-system connections from planning through final acceptance. Therefore, clients can control repairs, release work confidently, and maintain traceable records.

Piping quality depends on both workmanship and system control. Weld identity, material traceability, NDT status, pressure-test boundaries, and turnover records must agree. Because each project is different, we agree the inspection scope before work starts. We also identify witness points, hold points, reporting times, and responsible contacts.

Why piping welding inspection and NDT Guyana Matters

Welded joints often become part of a larger safety system. A single nonconforming joint can delay testing, coating, shipment, or start-up. However, early inspection keeps small problems from becoming expensive site repairs. It also gives production teams useful feedback while correction remains practical.

Common risks include wrong material, poor root condition, incomplete penetration, and uncontrolled repairs. Projects may also face missed NDT or test-pack delays. Therefore, our inspectors review both the physical work and the records that support it. This balanced approach protects quality without creating unnecessary delay.

Inspection Before Welding Starts

Before production starts, the inspector checks the latest drawings, specifications, and inspection plan. Material certificates and identification marks are compared with the required grade. In addition, welding consumables, storage controls, joint details, and welder qualifications are reviewed. The team then confirms that the correct approved procedure is available at the work area.

Fit-up receives close attention because preparation affects the entire joint. We check alignment, root opening, bevel condition, cleanliness, tack welds, and access. Where the procedure requires preheat, the inspector confirms the method and temperature range. Consequently, the welder begins with a controlled and documented joint.

Weld Surveillance and Visual Testing

While production continues, our inspector monitors technique and essential variables within the agreed scope. These may include amperage, voltage, travel speed, heat input, interpass temperature, shielding, and consumable control. The inspector also watches bead placement, cleaning, and joint sequence. If a deviation appears, it can be addressed before the joint progresses further.

At final inspection, visual testing checks profile, size, contour, surface condition, and visible discontinuities. The result is compared with the governing acceptance criteria. The inspection may also confirm dimensions, identification, and readiness for the next activity. Therefore, coating, NDT, pressure testing, or shipment does not begin with unresolved quality questions.

Typical Checks and NDT Support

Kheeran Offshore tailors the inspection plan to the joint design, material, access, and code. Typical activities include:

  • wrong material prevention and material traceability checks;
  • fit-up and weld inspection against approved drawings and procedures;
  • PT or MT for surface testing during agreed witness points;
  • UT where required using the specified acceptance criteria;
  • PMI and document verification and repair verification; and
  • final status review before release or turnover.

Non-destructive testing must suit the expected discontinuity and the applicable requirement. Visual testing supports every weld examination. In addition, liquid penetrant or magnetic particle testing can evaluate suitable surfaces. Ultrasonic testing may examine internal conditions when the geometry and code allow it. We coordinate the required method and confirm that results link to the correct weld.

Codes, Procedures, and Acceptance Criteria

Inspection follows ASME B31.3, ASME Section IX, API 1104 where relevant, and the approved project specification. The contract documents always control the final scope and acceptance limits. Therefore, our inspector confirms the required code edition and project amendments before making acceptance decisions. Qualification records are also checked against the essential variables of the planned work.

Kheeran Offshore can review WPS, PQR, and welder performance qualification documents. When required, we witness qualification testing and verify test identification. We also track repairs to the approved repair procedure. This disciplined process helps prevent informal changes that weaken traceability or delay handover.

Clear Reporting for Project Decisions

Useful inspection reports should tell the project team what was checked, where it was checked, and what happened next. Our reporting may include weld maps, NDT reports, repair registers, test-pack support, and final acceptance records. Findings identify the relevant weld, drawing, specification, and acceptance clause whenever practical. As a result, responsible teams can act without guessing.

Open items remain visible until the agreed disposition is complete. Repairs receive a new inspection and the required NDT. Then, the records show whether the item is accepted, rejected, or awaiting action. This simple status control supports fabrication meetings, turnover reviews, and client audits.

Local Support from Kheeran Offshore Guyana

Local coordination matters when schedules change quickly. Kheeran Offshore is based in Georgetown and can support fabrication yards, construction sites, industrial facilities, and offshore assignments. Our team communicates promptly with project personnel while maintaining independent technical judgment. Therefore, clients receive responsive service without reducing inspection discipline.

Our piping welding inspection and NDT Guyana can support one inspection visit or an ongoing quality assignment. We can work to an existing inspection test plan or help define practical surveillance points. In either case, the objective remains the same: verify compliant work, reduce avoidable rework, and protect people, equipment, and schedules.

Request Piping Welding Inspection and NDT Guyana

Discuss your next project with Kheeran Offshore. Call or WhatsApp +592-602-5664, email admin@kheeran.gy, or visit our contact page. Share the project location, code, material, joint type, schedule, and required inspection points. We will review the scope and provide a clear quotation for piping welding inspection and NDT Guyana.

by Kheeran Offshore Technical Team Kheeran Offshore Technical Team

Welding Inspection Services for FPSO in Guyana

Kheeran Offshore provides FPSO welding inspection Guyana for FPSO process piping, structural steel, modules, supports, and maintenance repairs. Our independent inspectors support FPSO operators, offshore contractors, module yards, and integrity teams. They verify work against the approved code, drawings, specifications, and welding procedure. As a result, quality issues can be found before they affect installation or commissioning.

An FPSO brings many welding codes and asset systems into one project. Inspection must identify the governing requirement for each joint before production begins. Because each project is different, we agree the inspection scope before work starts. We also identify witness points, hold points, reporting times, and responsible contacts.

Why FPSO welding inspection Guyana Matters

Welded joints often become part of a larger safety system. A single nonconforming joint can delay testing, coating, shipment, or start-up. However, early inspection keeps small problems from becoming expensive site repairs. It also gives production teams useful feedback while correction remains practical.

Common risks include code misapplication, material mix-up, repair growth, and restricted access. Projects may also face late NDT or handover gaps. Therefore, our inspectors review both the physical work and the records that support it. This balanced approach protects quality without creating unnecessary delay.

Inspection Before Welding Starts

First, the inspector checks the latest drawings, specifications, and inspection plan. Material certificates and identification marks are compared with the required grade. In addition, welding consumables, storage controls, joint details, and welder qualifications are reviewed. The team then confirms that the correct approved procedure is available at the work area.

Fit-up receives close attention because preparation affects the entire joint. We check alignment, root opening, bevel condition, cleanliness, tack welds, and access. Where the procedure requires preheat, the inspector confirms the method and temperature range. Consequently, the welder begins with a controlled and documented joint.

Weld Surveillance and Visual Testing

During welding, our inspector monitors technique and essential variables within the agreed scope. These may include amperage, voltage, travel speed, heat input, interpass temperature, shielding, and consumable control. The inspector also watches bead placement, cleaning, and joint sequence. If a deviation appears, it can be addressed before the joint progresses further.

After welding, visual testing checks profile, size, contour, surface condition, and visible discontinuities. The result is compared with the governing acceptance criteria. The inspection may also confirm dimensions, identification, and readiness for the next activity. Therefore, coating, NDT, pressure testing, or shipment does not begin with unresolved quality questions.

Typical Checks and NDT Support

Kheeran Offshore tailors the inspection plan to the joint design, material, access, and code. Typical activities include:

  • code misapplication prevention and material traceability checks;
  • scope and code review against approved drawings and procedures;
  • material verification during agreed witness points;
  • weld surveillance using the specified acceptance criteria;
  • NDT and repair follow-up and repair verification; and
  • final status review before release or turnover.

Non-destructive testing must suit the expected discontinuity and the applicable requirement. Visual testing supports every weld examination. In addition, liquid penetrant or magnetic particle testing can evaluate suitable surfaces. Ultrasonic testing may examine internal conditions when the geometry and code allow it. We coordinate the required method and confirm that results link to the correct weld.

Codes, Procedures, and Acceptance Criteria

Inspection follows the approved ASME, AWS, API, class, or owner requirement assigned to each system. The contract documents always control the final scope and acceptance limits. Therefore, our inspector confirms the required code edition and project amendments before making acceptance decisions. Qualification records are also checked against the essential variables of the planned work.

Kheeran Offshore can review WPS, PQR, and welder performance qualification documents. When required, we witness qualification testing and verify test identification. We also track repairs to the approved repair procedure. This disciplined process helps prevent informal changes that weaken traceability or delay handover.

Clear Reporting for Project Decisions

Useful inspection reports should tell the project team what was checked, where it was checked, and what happened next. Our reporting may include system-based reports, weld and repair status, NDT traceability, punch closure, and turnover support. Findings identify the relevant weld, drawing, specification, and acceptance clause whenever practical. As a result, responsible teams can act without guessing.

Open items remain visible until the agreed disposition is complete. Repairs receive a new inspection and the required NDT. Then, the records show whether the item is accepted, rejected, or awaiting action. This simple status control supports fabrication meetings, turnover reviews, and client audits.

Local Support from Kheeran Offshore Guyana

Local coordination matters when schedules change quickly. Kheeran Offshore is based in Georgetown and can support fabrication yards, construction sites, industrial facilities, and offshore assignments. Our team communicates promptly with project personnel while maintaining independent technical judgment. Therefore, clients receive responsive service without reducing inspection discipline.

Our FPSO welding inspection Guyana can support one inspection visit or an ongoing quality assignment. We can work to an existing inspection test plan or help define practical surveillance points. In either case, the objective remains the same: verify compliant work, reduce avoidable rework, and protect people, equipment, and schedules.

Request Welding Inspection Services for FPSO in Guyana

Discuss your next project with Kheeran Offshore. Call or WhatsApp +592-602-5664, email admin@kheeran.gy, or visit our contact page. Share the project location, code, material, joint type, schedule, and required inspection points. We will review the scope and provide a clear quotation for FPSO welding inspection Guyana.

by Kheeran Offshore Technical Team Kheeran Offshore Technical Team

Welding Inspection for Offshore Facilities as per AWS Standards in Guyana

Projects use offshore welding inspection Guyana when welded work needs an objective technical review. Kheeran Offshore inspects offshore modules, marine structures, platforms, skids, and support steel for offshore fabricators, marine contractors, operators, and engineering teams. Our work links field observations with the approved quality documents. Consequently, acceptance decisions remain consistent and auditable.

Offshore structures combine high consequence with restricted access. Early inspection is therefore valuable because a shop repair is simpler than offshore correction after installation. Because each project is different, we agree the inspection scope before work starts. We also identify witness points, hold points, reporting times, and responsible contacts.

Why offshore welding inspection Guyana Matters

Welded joints often become part of a larger safety system. A single nonconforming joint can delay testing, coating, shipment, or start-up. However, early inspection keeps small problems from becoming expensive site repairs. It also gives production teams useful feedback while correction remains practical.

Common risks include fatigue-critical defects, wrong joint details, environmental exposure, and poor repair access. Projects may also face coating delays or incomplete traceability. Therefore, our inspectors review both the physical work and the records that support it. This balanced approach protects quality without creating unnecessary delay.

Inspection Before Welding Starts

At the planning stage, the inspector checks the latest drawings, specifications, and inspection plan. Material certificates and identification marks are compared with the required grade. In addition, welding consumables, storage controls, joint details, and welder qualifications are reviewed. The team then confirms that the correct approved procedure is available at the work area.

Fit-up receives close attention because preparation affects the entire joint. We check alignment, root opening, bevel condition, cleanliness, tack welds, and access. Where the procedure requires preheat, the inspector confirms the method and temperature range. Consequently, the welder begins with a controlled and documented joint.

Weld Surveillance and Visual Testing

Once welding begins, our inspector monitors technique and essential variables within the agreed scope. These may include amperage, voltage, travel speed, heat input, interpass temperature, shielding, and consumable control. The inspector also watches bead placement, cleaning, and joint sequence. If a deviation appears, it can be addressed before the joint progresses further.

When the joint is complete, visual testing checks profile, size, contour, surface condition, and visible discontinuities. The result is compared with the governing acceptance criteria. The inspection may also confirm dimensions, identification, and readiness for the next activity. Therefore, coating, NDT, pressure testing, or shipment does not begin with unresolved quality questions.

Typical Checks and NDT Support

Kheeran Offshore tailors the inspection plan to the joint design, material, access, and code. Typical activities include:

  • fatigue-critical defects prevention and material traceability checks;
  • AWS document review against approved drawings and procedures;
  • fit-up and welding surveillance during agreed witness points;
  • visual testing using the specified acceptance criteria;
  • verification of NDT and repairs and repair verification; and
  • final status review before release or turnover.

Non-destructive testing must suit the expected discontinuity and the applicable requirement. Visual testing supports every weld examination. In addition, liquid penetrant or magnetic particle testing can evaluate suitable surfaces. Ultrasonic testing may examine internal conditions when the geometry and code allow it. We coordinate the required method and confirm that results link to the correct weld.

Codes, Procedures, and Acceptance Criteria

Inspection follows AWS D1.1 where contractually applicable, project specifications, approved drawings, and client-defined offshore requirements. The contract documents always control the final scope and acceptance limits. Therefore, our inspector confirms the required code edition and project amendments before making acceptance decisions. Qualification records are also checked against the essential variables of the planned work.

Kheeran Offshore can review WPS, PQR, and welder performance qualification documents. When required, we witness qualification testing and verify test identification. We also track repairs to the approved repair procedure. This disciplined process helps prevent informal changes that weaken traceability or delay handover.

Clear Reporting for Project Decisions

Useful inspection reports should tell the project team what was checked, where it was checked, and what happened next. Our reporting may include hold-point records, weld maps, NDT status, repair closure, and fabrication release documentation. Findings identify the relevant weld, drawing, specification, and acceptance clause whenever practical. As a result, responsible teams can act without guessing.

Open items remain visible until the agreed disposition is complete. Repairs receive a new inspection and the required NDT. Then, the records show whether the item is accepted, rejected, or awaiting action. This simple status control supports fabrication meetings, turnover reviews, and client audits.

Local Support from Kheeran Offshore Guyana

Local coordination matters when schedules change quickly. Kheeran Offshore is based in Georgetown and can support fabrication yards, construction sites, industrial facilities, and offshore assignments. Our team communicates promptly with project personnel while maintaining independent technical judgment. Therefore, clients receive responsive service without reducing inspection discipline.

Our offshore welding inspection Guyana can support one inspection visit or an ongoing quality assignment. We can work to an existing inspection test plan or help define practical surveillance points. In either case, the objective remains the same: verify compliant work, reduce avoidable rework, and protect people, equipment, and schedules.

Request Welding Inspection for Offshore Facilities as per AWS Standards in Guyana

Discuss your next project with Kheeran Offshore. Call or WhatsApp +592-602-5664, email admin@kheeran.gy, or visit our contact page. Share the project location, code, material, joint type, schedule, and required inspection points. We will review the scope and provide a clear quotation for offshore welding inspection Guyana.

by Kheeran Offshore Technical Team Kheeran Offshore Technical Team

Pipeline Welding Inspection Services in Guyana

Reliable pipeline welding inspection Guyana gives project teams clear evidence about weld quality. Kheeran Offshore supports pipeline contractors, operators, EPC teams, and construction quality managers across Guyana. We inspect cross-country pipelines, facility tie-ins, field welds, repairs, and associated piping from planning through final acceptance. Therefore, clients can control repairs, release work confidently, and maintain traceable records.

Pipeline production moves in a sequence, so one missed control can travel with the spread. Timely inspection keeps materials, welder identity, parameters, NDT, and repairs connected. Because each project is different, we agree the inspection scope before work starts. We also identify witness points, hold points, reporting times, and responsible contacts.

Why pipeline welding inspection Guyana Matters

Welded joints often become part of a larger safety system. A single nonconforming joint can delay testing, coating, shipment, or start-up. However, early inspection keeps small problems from becoming expensive site repairs. It also gives production teams useful feedback while correction remains practical.

Common risks include incorrect alignment, hydrogen cracking, parameter drift, and poor tie-in control. Projects may also face repair accumulation or traceability loss. Therefore, our inspectors review both the physical work and the records that support it. This balanced approach protects quality without creating unnecessary delay.

Inspection Before Welding Starts

Before production starts, the inspector checks the latest drawings, specifications, and inspection plan. Material certificates and identification marks are compared with the required grade. In addition, welding consumables, storage controls, joint details, and welder qualifications are reviewed. The team then confirms that the correct approved procedure is available at the work area.

Fit-up receives close attention because preparation affects the entire joint. We check alignment, root opening, bevel condition, cleanliness, tack welds, and access. Where the procedure requires preheat, the inspector confirms the method and temperature range. Consequently, the welder begins with a controlled and documented joint.

Weld Surveillance and Visual Testing

While production continues, our inspector monitors technique and essential variables within the agreed scope. These may include amperage, voltage, travel speed, heat input, interpass temperature, shielding, and consumable control. The inspector also watches bead placement, cleaning, and joint sequence. If a deviation appears, it can be addressed before the joint progresses further.

At final inspection, visual testing checks profile, size, contour, surface condition, and visible discontinuities. The result is compared with the governing acceptance criteria. The inspection may also confirm dimensions, identification, and readiness for the next activity. Therefore, coating, NDT, pressure testing, or shipment does not begin with unresolved quality questions.

Typical Checks and NDT Support

Kheeran Offshore tailors the inspection plan to the joint design, material, access, and code. Typical activities include:

  • incorrect alignment prevention and material traceability checks;
  • fit-up and root inspection against approved drawings and procedures;
  • parameter surveillance during agreed witness points;
  • visual examination using the specified acceptance criteria;
  • review of radiographic or ultrasonic results and repair verification; and
  • final status review before release or turnover.

Non-destructive testing must suit the expected discontinuity and the applicable requirement. Visual testing supports every weld examination. In addition, liquid penetrant or magnetic particle testing can evaluate suitable surfaces. Ultrasonic testing may examine internal conditions when the geometry and code allow it. We coordinate the required method and confirm that results link to the correct weld.

Codes, Procedures, and Acceptance Criteria

Inspection follows API 1104, ASME B31 requirements where specified, approved procedures, and the project pipeline quality plan. The contract documents always control the final scope and acceptance limits. Therefore, our inspector confirms the required code edition and project amendments before making acceptance decisions. Qualification records are also checked against the essential variables of the planned work.

Kheeran Offshore can review WPS, PQR, and welder performance qualification documents. When required, we witness qualification testing and verify test identification. We also track repairs to the approved repair procedure. This disciplined process helps prevent informal changes that weaken traceability or delay handover.

Clear Reporting for Project Decisions

Useful inspection reports should tell the project team what was checked, where it was checked, and what happened next. Our reporting may include weld-number records, daily summaries, NDT status, repair tracking, and completion dossiers. Findings identify the relevant weld, drawing, specification, and acceptance clause whenever practical. As a result, responsible teams can act without guessing.

Open items remain visible until the agreed disposition is complete. Repairs receive a new inspection and the required NDT. Then, the records show whether the item is accepted, rejected, or awaiting action. This simple status control supports fabrication meetings, turnover reviews, and client audits.

Local Support from Kheeran Offshore Guyana

Local coordination matters when schedules change quickly. Kheeran Offshore is based in Georgetown and can support fabrication yards, construction sites, industrial facilities, and offshore assignments. Our team communicates promptly with project personnel while maintaining independent technical judgment. Therefore, clients receive responsive service without reducing inspection discipline.

Our pipeline welding inspection Guyana can support one inspection visit or an ongoing quality assignment. We can work to an existing inspection test plan or help define practical surveillance points. In either case, the objective remains the same: verify compliant work, reduce avoidable rework, and protect people, equipment, and schedules.

Request Pipeline Welding Inspection Guyana

Discuss your next project with Kheeran Offshore. Call or WhatsApp +592-602-5664, email admin@kheeran.gy, or visit our contact page. Share the project location, code, material, joint type, schedule, and required inspection points. We will review the scope and provide a clear quotation for pipeline welding inspection Guyana.

by Kheeran Offshore Technical Team Kheeran Offshore Technical Team

Structural Steel Welding Inspection Services in Guyana

Kheeran Offshore provides structural steel welding inspection Guyana for platforms, modules, skids, buildings, pipe supports, and fabricated steelwork. Our independent inspectors support fabrication shops, construction contractors, module builders, and project owners. They verify work against the approved code, drawings, specifications, and welding procedure. As a result, quality issues can be found before they affect installation or commissioning.

Steel assemblies depend on thousands of small details working together. An inspection plan connects material certificates, joint preparation, welding control, final geometry, and release. Because each project is different, we agree the inspection scope before work starts. We also identify witness points, hold points, reporting times, and responsible contacts.

Why structural steel welding inspection Guyana Matters

Welded joints often become part of a larger safety system. A single nonconforming joint can delay testing, coating, shipment, or start-up. However, early inspection keeps small problems from becoming expensive site repairs. It also gives production teams useful feedback while correction remains practical.

Common risks include wrong steel grade, incorrect weld size, excessive distortion, and poor access for NDT. Projects may also face unapproved repairs or missing weld maps. Therefore, our inspectors review both the physical work and the records that support it. This balanced approach protects quality without creating unnecessary delay.

Inspection Before Welding Starts

First, the inspector checks the latest drawings, specifications, and inspection plan. Material certificates and identification marks are compared with the required grade. In addition, welding consumables, storage controls, joint details, and welder qualifications are reviewed. The team then confirms that the correct approved procedure is available at the work area.

Fit-up receives close attention because preparation affects the entire joint. We check alignment, root opening, bevel condition, cleanliness, tack welds, and access. Where the procedure requires preheat, the inspector confirms the method and temperature range. Consequently, the welder begins with a controlled and documented joint.

Weld Surveillance and Visual Testing

During welding, our inspector monitors technique and essential variables within the agreed scope. These may include amperage, voltage, travel speed, heat input, interpass temperature, shielding, and consumable control. The inspector also watches bead placement, cleaning, and joint sequence. If a deviation appears, it can be addressed before the joint progresses further.

After welding, visual testing checks profile, size, contour, surface condition, and visible discontinuities. The result is compared with the governing acceptance criteria. The inspection may also confirm dimensions, identification, and readiness for the next activity. Therefore, coating, NDT, pressure testing, or shipment does not begin with unresolved quality questions.

Typical Checks and NDT Support

Kheeran Offshore tailors the inspection plan to the joint design, material, access, and code. Typical activities include:

  • wrong steel grade prevention and material traceability checks;
  • material and drawing review against approved drawings and procedures;
  • fit-up inspection during agreed witness points;
  • in-process surveillance using the specified acceptance criteria;
  • final VT and NDT review and repair verification; and
  • final status review before release or turnover.

Non-destructive testing must suit the expected discontinuity and the applicable requirement. Visual testing supports every weld examination. In addition, liquid penetrant or magnetic particle testing can evaluate suitable surfaces. Ultrasonic testing may examine internal conditions when the geometry and code allow it. We coordinate the required method and confirm that results link to the correct weld.

Codes, Procedures, and Acceptance Criteria

Inspection follows AWS D1.1, client structural specifications, approved WPS documents, and project inspection plans. The contract documents always control the final scope and acceptance limits. Therefore, our inspector confirms the required code edition and project amendments before making acceptance decisions. Qualification records are also checked against the essential variables of the planned work.

Kheeran Offshore can review WPS, PQR, and welder performance qualification documents. When required, we witness qualification testing and verify test identification. We also track repairs to the approved repair procedure. This disciplined process helps prevent informal changes that weaken traceability or delay handover.

Clear Reporting for Project Decisions

Useful inspection reports should tell the project team what was checked, where it was checked, and what happened next. Our reporting may include weld traceability, dimensional results, inspection releases, nonconformance control, and a final quality package. Findings identify the relevant weld, drawing, specification, and acceptance clause whenever practical. As a result, responsible teams can act without guessing.

Open items remain visible until the agreed disposition is complete. Repairs receive a new inspection and the required NDT. Then, the records show whether the item is accepted, rejected, or awaiting action. This simple status control supports fabrication meetings, turnover reviews, and client audits.

Local Support from Kheeran Offshore Guyana

Local coordination matters when schedules change quickly. Kheeran Offshore is based in Georgetown and can support fabrication yards, construction sites, industrial facilities, and offshore assignments. Our team communicates promptly with project personnel while maintaining independent technical judgment. Therefore, clients receive responsive service without reducing inspection discipline.

Our structural steel welding inspection Guyana can support one inspection visit or an ongoing quality assignment. We can work to an existing inspection test plan or help define practical surveillance points. In either case, the objective remains the same: verify compliant work, reduce avoidable rework, and protect people, equipment, and schedules.

Request Structural Steel Welding Inspection Guyana

Discuss your next project with Kheeran Offshore. Call or WhatsApp +592-602-5664, email admin@kheeran.gy, or visit our contact page. Share the project location, code, material, joint type, schedule, and required inspection points. We will review the scope and provide a clear quotation for structural steel welding inspection Guyana.

by Kheeran Offshore Technical Team Kheeran Offshore Technical Team

Piers and Bridges Welding Inspection Services in Guyana

Projects use bridge welding inspection Guyana when welded work needs an objective technical review. Kheeran Offshore inspects bridge members, pier steelwork, marine connections, supports, and repair areas for civil contractors, infrastructure owners, steel fabricators, and consulting engineers. Our work links field observations with the approved quality documents. Consequently, acceptance decisions remain consistent and auditable.

Bridge and pier welds face demanding service and exposure. Inspection must follow the approved design while also considering access, sequence, distortion, and repair control. Because each project is different, we agree the inspection scope before work starts. We also identify witness points, hold points, reporting times, and responsible contacts.

Why bridge welding inspection Guyana Matters

Welded joints often become part of a larger safety system. A single nonconforming joint can delay testing, coating, shipment, or start-up. However, early inspection keeps small problems from becoming expensive site repairs. It also gives production teams useful feedback while correction remains practical.

Common risks include fatigue-sensitive discontinuities, incorrect weld profiles, misalignment, and lamellar concerns. Projects may also face uncontrolled field repairs or record gaps. Therefore, our inspectors review both the physical work and the records that support it. This balanced approach protects quality without creating unnecessary delay.

Inspection Before Welding Starts

At the planning stage, the inspector checks the latest drawings, specifications, and inspection plan. Material certificates and identification marks are compared with the required grade. In addition, welding consumables, storage controls, joint details, and welder qualifications are reviewed. The team then confirms that the correct approved procedure is available at the work area.

Fit-up receives close attention because preparation affects the entire joint. We check alignment, root opening, bevel condition, cleanliness, tack welds, and access. Where the procedure requires preheat, the inspector confirms the method and temperature range. Consequently, the welder begins with a controlled and documented joint.

Weld Surveillance and Visual Testing

Once welding begins, our inspector monitors technique and essential variables within the agreed scope. These may include amperage, voltage, travel speed, heat input, interpass temperature, shielding, and consumable control. The inspector also watches bead placement, cleaning, and joint sequence. If a deviation appears, it can be addressed before the joint progresses further.

When the joint is complete, visual testing checks profile, size, contour, surface condition, and visible discontinuities. The result is compared with the governing acceptance criteria. The inspection may also confirm dimensions, identification, and readiness for the next activity. Therefore, coating, NDT, pressure testing, or shipment does not begin with unresolved quality questions.

Typical Checks and NDT Support

Kheeran Offshore tailors the inspection plan to the joint design, material, access, and code. Typical activities include:

  • fatigue-sensitive discontinuities prevention and material traceability checks;
  • fabrication surveillance against approved drawings and procedures;
  • site visual inspection during agreed witness points;
  • dimensional checks using the specified acceptance criteria;
  • coordination of MT, PT, or UT and repair verification; and
  • final status review before release or turnover.

Non-destructive testing must suit the expected discontinuity and the applicable requirement. Visual testing supports every weld examination. In addition, liquid penetrant or magnetic particle testing can evaluate suitable surfaces. Ultrasonic testing may examine internal conditions when the geometry and code allow it. We coordinate the required method and confirm that results link to the correct weld.

Codes, Procedures, and Acceptance Criteria

Inspection follows AWS D1.1 or the project bridge specification, approved drawings, welding procedures, and engineer-defined acceptance criteria. The contract documents always control the final scope and acceptance limits. Therefore, our inspector confirms the required code edition and project amendments before making acceptance decisions. Qualification records are also checked against the essential variables of the planned work.

Kheeran Offshore can review WPS, PQR, and welder performance qualification documents. When required, we witness qualification testing and verify test identification. We also track repairs to the approved repair procedure. This disciplined process helps prevent informal changes that weaken traceability or delay handover.

Clear Reporting for Project Decisions

Useful inspection reports should tell the project team what was checked, where it was checked, and what happened next. Our reporting may include location-based weld records, repair logs, NDT reports, punch lists, and acceptance summaries. Findings identify the relevant weld, drawing, specification, and acceptance clause whenever practical. As a result, responsible teams can act without guessing.

Open items remain visible until the agreed disposition is complete. Repairs receive a new inspection and the required NDT. Then, the records show whether the item is accepted, rejected, or awaiting action. This simple status control supports fabrication meetings, turnover reviews, and client audits.

Local Support from Kheeran Offshore Guyana

Local coordination matters when schedules change quickly. Kheeran Offshore is based in Georgetown and can support fabrication yards, construction sites, industrial facilities, and offshore assignments. Our team communicates promptly with project personnel while maintaining independent technical judgment. Therefore, clients receive responsive service without reducing inspection discipline.

Our bridge welding inspection Guyana can support one inspection visit or an ongoing quality assignment. We can work to an existing inspection test plan or help define practical surveillance points. In either case, the objective remains the same: verify compliant work, reduce avoidable rework, and protect people, equipment, and schedules.

Request Piers and Bridges Welding Inspection Guyana

Discuss your next project with Kheeran Offshore. Call or WhatsApp +592-602-5664, email admin@kheeran.gy, or visit our contact page. Share the project location, code, material, joint type, schedule, and required inspection points. We will review the scope and provide a clear quotation for bridge welding inspection Guyana.

by Kheeran Offshore Technical Team Kheeran Offshore Technical Team

Visual Weld Inspection Before Non-Destructive Testing

Visual Weld Inspection Before Non-Destructive Testing focuses on one defined technical question. Visual examination should confirm weld profile, dimensions, surface condition and obvious discontinuities before more specialised NDT is scheduled.

A practical inspection plan defines the stage, drawing, weld or component identity, method, acceptance criteria, hold points and reporting responsibility. Findings, repairs and reinspection should remain traceable through final close-out.

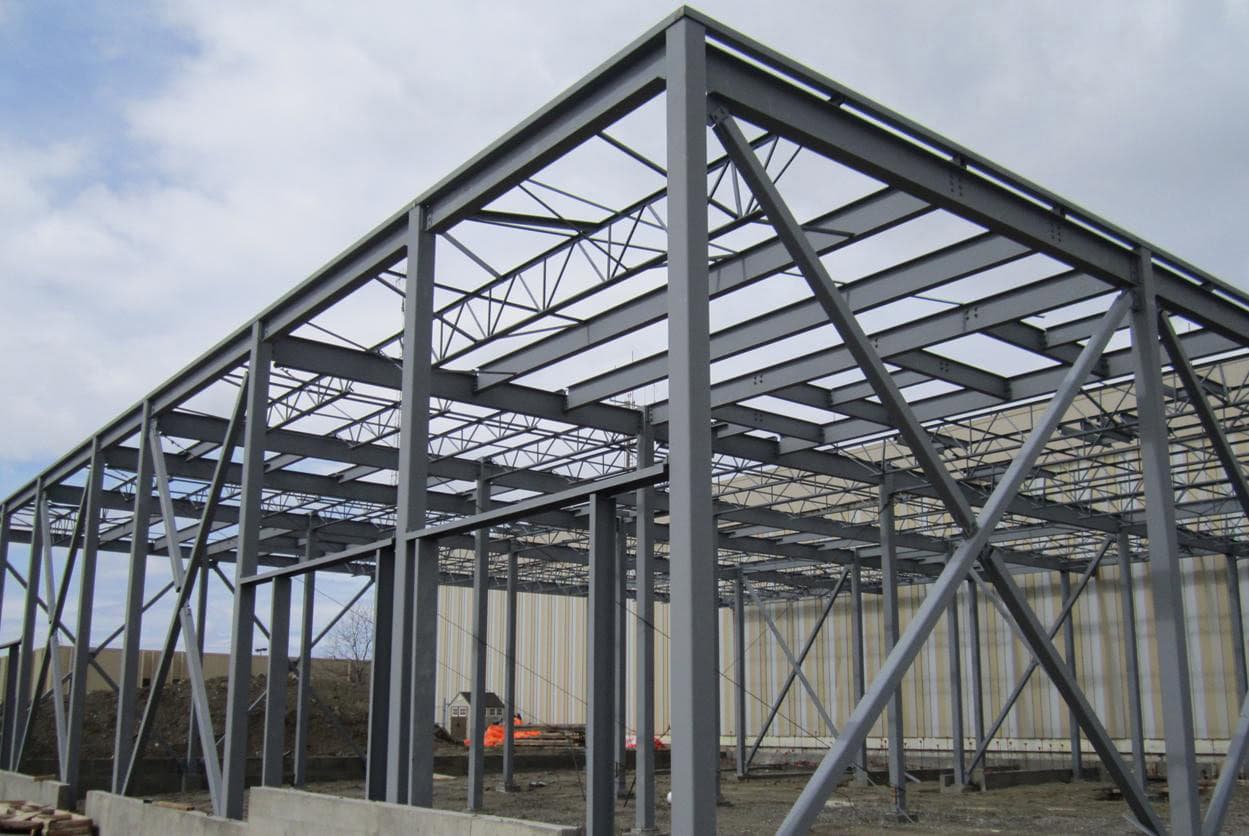
Reliable structural steel inspection Georgetown gives project teams clear evidence about weld quality. Kheeran Offshore supports steel fabricators, building contractors, engineering firms, and project owners across Guyana. We inspect frames, platforms, skids, supports, stairs, and other structural assemblies from planning through final acceptance. Therefore, clients can control repairs, release work confidently, and maintain traceable records.

Structural quality involves more than the weld bead. Member orientation, dimensions, connection details, bolt installation, and coating readiness also affect final fit and service. Because each project is different, we agree the inspection scope before work starts. We also identify witness points, hold points, reporting times, and responsible contacts.

Why structural steel inspection Georgetown Matters

Welded joints often become part of a larger safety system. A single nonconforming joint can delay testing, coating, shipment, or start-up. However, early inspection keeps small problems from becoming expensive site repairs. It also gives production teams useful feedback while correction remains practical.

Common risks include member misalignment, incorrect connection details, weld size errors, and distortion. Projects may also face missing identification or premature coating. Therefore, our inspectors review both the physical work and the records that support it. This balanced approach protects quality without creating unnecessary delay.

Inspection Before Welding Starts

Before production starts, the inspector checks the latest drawings, specifications, and inspection plan. Material certificates and identification marks are compared with the required grade. In addition, welding consumables, storage controls, joint details, and welder qualifications are reviewed. The team then confirms that the correct approved procedure is available at the work area.

Fit-up receives close attention because preparation affects the entire joint. We check alignment, root opening, bevel condition, cleanliness, tack welds, and access. Where the procedure requires preheat, the inspector confirms the method and temperature range. Consequently, the welder begins with a controlled and documented joint.

Weld Surveillance and Visual Testing

While production continues, our inspector monitors technique and essential variables within the agreed scope. These may include amperage, voltage, travel speed, heat input, interpass temperature, shielding, and consumable control. The inspector also watches bead placement, cleaning, and joint sequence. If a deviation appears, it can be addressed before the joint progresses further.

At final inspection, visual testing checks profile, size, contour, surface condition, and visible discontinuities. The result is compared with the governing acceptance criteria. The inspection may also confirm dimensions, identification, and readiness for the next activity. Therefore, coating, NDT, pressure testing, or shipment does not begin with unresolved quality questions.

Typical Checks and NDT Support

Kheeran Offshore tailors the inspection plan to the joint design, material, access, and code. Typical activities include:

  • member misalignment prevention and material traceability checks;
  • drawing review against approved drawings and procedures;
  • dimensional inspection during agreed witness points;
  • visual weld testing using the specified acceptance criteria;
  • fabrication and erection surveillance and repair verification; and
  • final status review before release or turnover.

Non-destructive testing must suit the expected discontinuity and the applicable requirement. Visual testing supports every weld examination. In addition, liquid penetrant or magnetic particle testing can evaluate suitable surfaces. Ultrasonic testing may examine internal conditions when the geometry and code allow it. We coordinate the required method and confirm that results link to the correct weld.

Codes, Procedures, and Acceptance Criteria

Inspection follows AWS D1.1, approved structural drawings, project tolerances, and specified bolting or coating requirements. The contract documents always control the final scope and acceptance limits. Therefore, our inspector confirms the required code edition and project amendments before making acceptance decisions. Qualification records are also checked against the essential variables of the planned work.

Kheeran Offshore can review WPS, PQR, and welder performance qualification documents. When required, we witness qualification testing and verify test identification. We also track repairs to the approved repair procedure. This disciplined process helps prevent informal changes that weaken traceability or delay handover.

Clear Reporting for Project Decisions

Useful inspection reports should tell the project team what was checked, where it was checked, and what happened next. Our reporting may include dimensional records, weld findings, punch lists, repair verification, and release reports. Findings identify the relevant weld, drawing, specification, and acceptance clause whenever practical. As a result, responsible teams can act without guessing.

Open items remain visible until the agreed disposition is complete. Repairs receive a new inspection and the required NDT. Then, the records show whether the item is accepted, rejected, or awaiting action. This simple status control supports fabrication meetings, turnover reviews, and client audits.

Local Support from Kheeran Offshore Guyana

Local coordination matters when schedules change quickly. Kheeran Offshore is based in Georgetown and can support fabrication yards, construction sites, industrial facilities, and offshore assignments. Our team communicates promptly with project personnel while maintaining independent technical judgment. Therefore, clients receive responsive service without reducing inspection discipline.

Our structural steel inspection Georgetown can support one inspection visit or an ongoing quality assignment. We can work to an existing inspection test plan or help define practical surveillance points. In either case, the objective remains the same: verify compliant work, reduce avoidable rework, and protect people, equipment, and schedules.

Request Structural Steel Inspection Georgetown Guyana

Discuss your next project with Kheeran Offshore. Call or WhatsApp +592-602-5664, email admin@kheeran.gy, or visit our contact page. Share the project location, code, material, joint type, schedule, and required inspection points. We will review the scope and provide a clear quotation for structural steel inspection Georgetown.

by Kheeran Offshore Technical Team Kheeran Offshore Technical Team

Welding Inspection Services for FPSO Shutdown Projects in Guyana

Kheeran Offshore provides FPSO shutdown welding inspection Guyana for time-critical FPSO repairs, piping modifications, and structural renewals. Our independent inspectors support shutdown managers, offshore contractors, maintenance planners, and vessel quality teams. They verify work against the approved code, drawings, specifications, and welding procedure. As a result, quality issues can be found before they affect installation or commissioning.

A shutdown compresses many decisions into a short window. Inspection must move quickly, yet every repair still needs controlled materials, qualified procedures, and traceable acceptance. Because each project is different, we agree the inspection scope before work starts. We also identify witness points, hold points, reporting times, and responsible contacts.

Why FPSO shutdown welding inspection Guyana Matters

Welded joints often become part of a larger safety system. A single nonconforming joint can delay testing, coating, shipment, or start-up. However, early inspection keeps small problems from becoming expensive site repairs. It also gives production teams useful feedback while correction remains practical.

Common risks include schedule-driven shortcuts, incorrect repair preparation, mixed materials, and missed examinations. Projects may also face open punch items or incomplete turnover packs. Therefore, our inspectors review both the physical work and the records that support it. This balanced approach protects quality without creating unnecessary delay.

Inspection Before Welding Starts

First, the inspector checks the latest drawings, specifications, and inspection plan. Material certificates and identification marks are compared with the required grade. In addition, welding consumables, storage controls, joint details, and welder qualifications are reviewed. The team then confirms that the correct approved procedure is available at the work area.

Fit-up receives close attention because preparation affects the entire joint. We check alignment, root opening, bevel condition, cleanliness, tack welds, and access. Where the procedure requires preheat, the inspector confirms the method and temperature range. Consequently, the welder begins with a controlled and documented joint.

Weld Surveillance and Visual Testing

During welding, our inspector monitors technique and essential variables within the agreed scope. These may include amperage, voltage, travel speed, heat input, interpass temperature, shielding, and consumable control. The inspector also watches bead placement, cleaning, and joint sequence. If a deviation appears, it can be addressed before the joint progresses further.

After welding, visual testing checks profile, size, contour, surface condition, and visible discontinuities. The result is compared with the governing acceptance criteria. The inspection may also confirm dimensions, identification, and readiness for the next activity. Therefore, coating, NDT, pressure testing, or shipment does not begin with unresolved quality questions.

Typical Checks and NDT Support

Kheeran Offshore tailors the inspection plan to the joint design, material, access, and code. Typical activities include:

  • schedule-driven shortcuts prevention and material traceability checks;
  • repair-area verification against approved drawings and procedures;
  • continuous weld surveillance during agreed witness points;
  • NDT coordination using the specified acceptance criteria;
  • turnover dossier review and repair verification; and
  • final status review before release or turnover.

Non-destructive testing must suit the expected discontinuity and the applicable requirement. Visual testing supports every weld examination. In addition, liquid penetrant or magnetic particle testing can evaluate suitable surfaces. Ultrasonic testing may examine internal conditions when the geometry and code allow it. We coordinate the required method and confirm that results link to the correct weld.

Codes, Procedures, and Acceptance Criteria

Inspection follows class requirements, approved repair procedures, ASME or AWS criteria, and the asset owner’s shutdown quality plan. The contract documents always control the final scope and acceptance limits. Therefore, our inspector confirms the required code edition and project amendments before making acceptance decisions. Qualification records are also checked against the essential variables of the planned work.

Kheeran Offshore can review WPS, PQR, and welder performance qualification documents. When required, we witness qualification testing and verify test identification. We also track repairs to the approved repair procedure. This disciplined process helps prevent informal changes that weaken traceability or delay handover.

Clear Reporting for Project Decisions

Useful inspection reports should tell the project team what was checked, where it was checked, and what happened next. Our reporting may include shift reports, repair status boards, NDT follow-up, punch-list closure, and turnover evidence. Findings identify the relevant weld, drawing, specification, and acceptance clause whenever practical. As a result, responsible teams can act without guessing.

Open items remain visible until the agreed disposition is complete. Repairs receive a new inspection and the required NDT. Then, the records show whether the item is accepted, rejected, or awaiting action. This simple status control supports fabrication meetings, turnover reviews, and client audits.

Local Support from Kheeran Offshore Guyana

Local coordination matters when schedules change quickly. Kheeran Offshore is based in Georgetown and can support fabrication yards, construction sites, industrial facilities, and offshore assignments. Our team communicates promptly with project personnel while maintaining independent technical judgment. Therefore, clients receive responsive service without reducing inspection discipline.

Our FPSO shutdown welding inspection Guyana can support one inspection visit or an ongoing quality assignment. We can work to an existing inspection test plan or help define practical surveillance points. In either case, the objective remains the same: verify compliant work, reduce avoidable rework, and protect people, equipment, and schedules.

Request Welding Inspection Services for FPSO Shutdown Projects in Guyana

Discuss your next project with Kheeran Offshore. Call or WhatsApp +592-602-5664, email admin@kheeran.gy, or visit our contact page. Share the project location, code, material, joint type, schedule, and required inspection points. We will review the scope and provide a clear quotation for FPSO shutdown welding inspection Guyana.

by Kheeran Offshore Technical Team Kheeran Offshore Technical Team

Coordinating Welding Inspection Across Guyana and Suriname

Coordinating Welding Inspection Across Guyana and Suriname focuses on one defined technical question. Multi-location projects need common inspection plans, reporting formats, document control and communication so acceptance decisions remain consistent.

A practical inspection plan defines the stage, drawing, weld or component identity, method, acceptance criteria, hold points and reporting responsibility. Findings, repairs and reinspection should remain traceable through final close-out.

Projects use Guyana and Suriname welding inspection when welded work needs an objective technical review. Kheeran Offshore inspects regional projects, vendors, marine facilities, and cross-border supply packages for operators, EPC contractors, procurement groups, and regional fabrication companies. Our work links field observations with the approved quality documents. Consequently, acceptance decisions remain consistent and auditable.

Regional projects need consistent acceptance decisions at every location. We align inspectors with one inspection plan, one reporting format, and one controlled document trail. Because each project is different, we agree the inspection scope before work starts. We also identify witness points, hold points, reporting times, and responsible contacts.

Why Guyana and Suriname welding inspection Matters

Welded joints often become part of a larger safety system. A single nonconforming joint can delay testing, coating, shipment, or start-up. However, early inspection keeps small problems from becoming expensive site repairs. It also gives production teams useful feedback while correction remains practical.

Common risks include inconsistent inspection criteria, regional vendor variation, document gaps, and handover delays. Projects may also face untracked repairs or different reporting formats. Therefore, our inspectors review both the physical work and the records that support it. This balanced approach protects quality without creating unnecessary delay.

Inspection Before Welding Starts

At the planning stage, the inspector checks the latest drawings, specifications, and inspection plan. Material certificates and identification marks are compared with the required grade. In addition, welding consumables, storage controls, joint details, and welder qualifications are reviewed. The team then confirms that the correct approved procedure is available at the work area.

Fit-up receives close attention because preparation affects the entire joint. We check alignment, root opening, bevel condition, cleanliness, tack welds, and access. Where the procedure requires preheat, the inspector confirms the method and temperature range. Consequently, the welder begins with a controlled and documented joint.

Weld Surveillance and Visual Testing

Once welding begins, our inspector monitors technique and essential variables within the agreed scope. These may include amperage, voltage, travel speed, heat input, interpass temperature, shielding, and consumable control. The inspector also watches bead placement, cleaning, and joint sequence. If a deviation appears, it can be addressed before the joint progresses further.

When the joint is complete, visual testing checks profile, size, contour, surface condition, and visible discontinuities. The result is compared with the governing acceptance criteria. The inspection may also confirm dimensions, identification, and readiness for the next activity. Therefore, coating, NDT, pressure testing, or shipment does not begin with unresolved quality questions.

Typical Checks and NDT Support

Kheeran Offshore tailors the inspection plan to the joint design, material, access, and code. Typical activities include:

  • inconsistent inspection criteria prevention and material traceability checks;
  • vendor inspection against approved drawings and procedures;
  • source surveillance during agreed witness points;
  • visual weld examination using the specified acceptance criteria;
  • review of qualification and NDT records and repair verification; and
  • final status review before release or turnover.

Non-destructive testing must suit the expected discontinuity and the applicable requirement. Visual testing supports every weld examination. In addition, liquid penetrant or magnetic particle testing can evaluate suitable surfaces. Ultrasonic testing may examine internal conditions when the geometry and code allow it. We coordinate the required method and confirm that results link to the correct weld.

Codes, Procedures, and Acceptance Criteria

Inspection follows the contractually selected AWS, ASME, API, or client standard and its approved project edition. The contract documents always control the final scope and acceptance limits. Therefore, our inspector confirms the required code edition and project amendments before making acceptance decisions. Qualification records are also checked against the essential variables of the planned work.

Kheeran Offshore can review WPS, PQR, and welder performance qualification documents. When required, we witness qualification testing and verify test identification. We also track repairs to the approved repair procedure. This disciplined process helps prevent informal changes that weaken traceability or delay handover.

Clear Reporting for Project Decisions

Useful inspection reports should tell the project team what was checked, where it was checked, and what happened next. Our reporting may include consistent regional reports, inspection release notes, open-item registers, and vendor status updates. Findings identify the relevant weld, drawing, specification, and acceptance clause whenever practical. As a result, responsible teams can act without guessing.

Open items remain visible until the agreed disposition is complete. Repairs receive a new inspection and the required NDT. Then, the records show whether the item is accepted, rejected, or awaiting action. This simple status control supports fabrication meetings, turnover reviews, and client audits.

Local Support from Kheeran Offshore Guyana

Local coordination matters when schedules change quickly. Kheeran Offshore is based in Georgetown and can support fabrication yards, construction sites, industrial facilities, and offshore assignments. Our team communicates promptly with project personnel while maintaining independent technical judgment. Therefore, clients receive responsive service without reducing inspection discipline.

Our Guyana and Suriname welding inspection can support one inspection visit or an ongoing quality assignment. We can work to an existing inspection test plan or help define practical surveillance points. In either case, the objective remains the same: verify compliant work, reduce avoidable rework, and protect people, equipment, and schedules.

Request Welding Inspection Guyana and Suriname

Discuss your next project with Kheeran Offshore. Call or WhatsApp +592-602-5664, email admin@kheeran.gy, or visit our contact page. Share the project location, code, material, joint type, schedule, and required inspection points. We will review the scope and provide a clear quotation for Guyana and Suriname welding inspection.